Publication number: ELQ-41704-1
View all versions & Certificate

SPC Excel Toolkit: Control Charts, Process Capability (Cpk) and Gage R&R
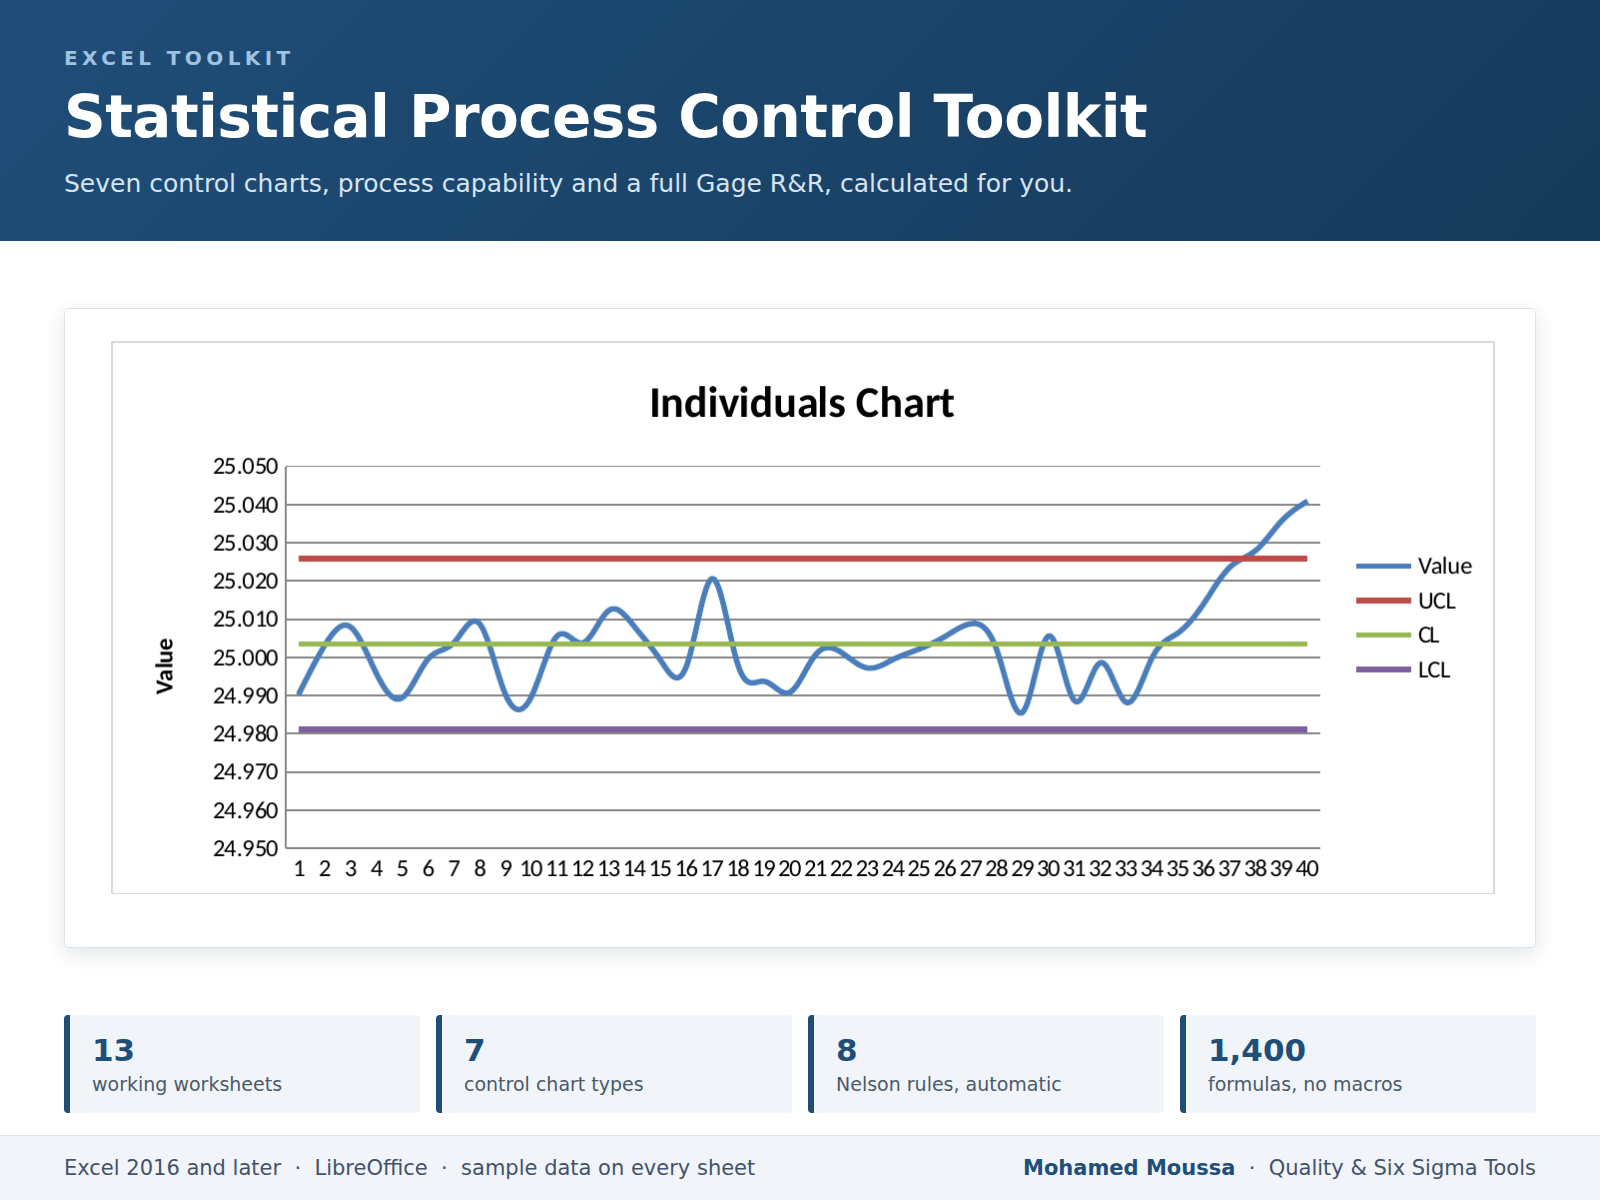
SPC that does the work: 7 control charts, capability and a full Gage R&R in one Excel workbook. No macros, sample data on every sheet.
Further information
After using this workbook you will be able to:
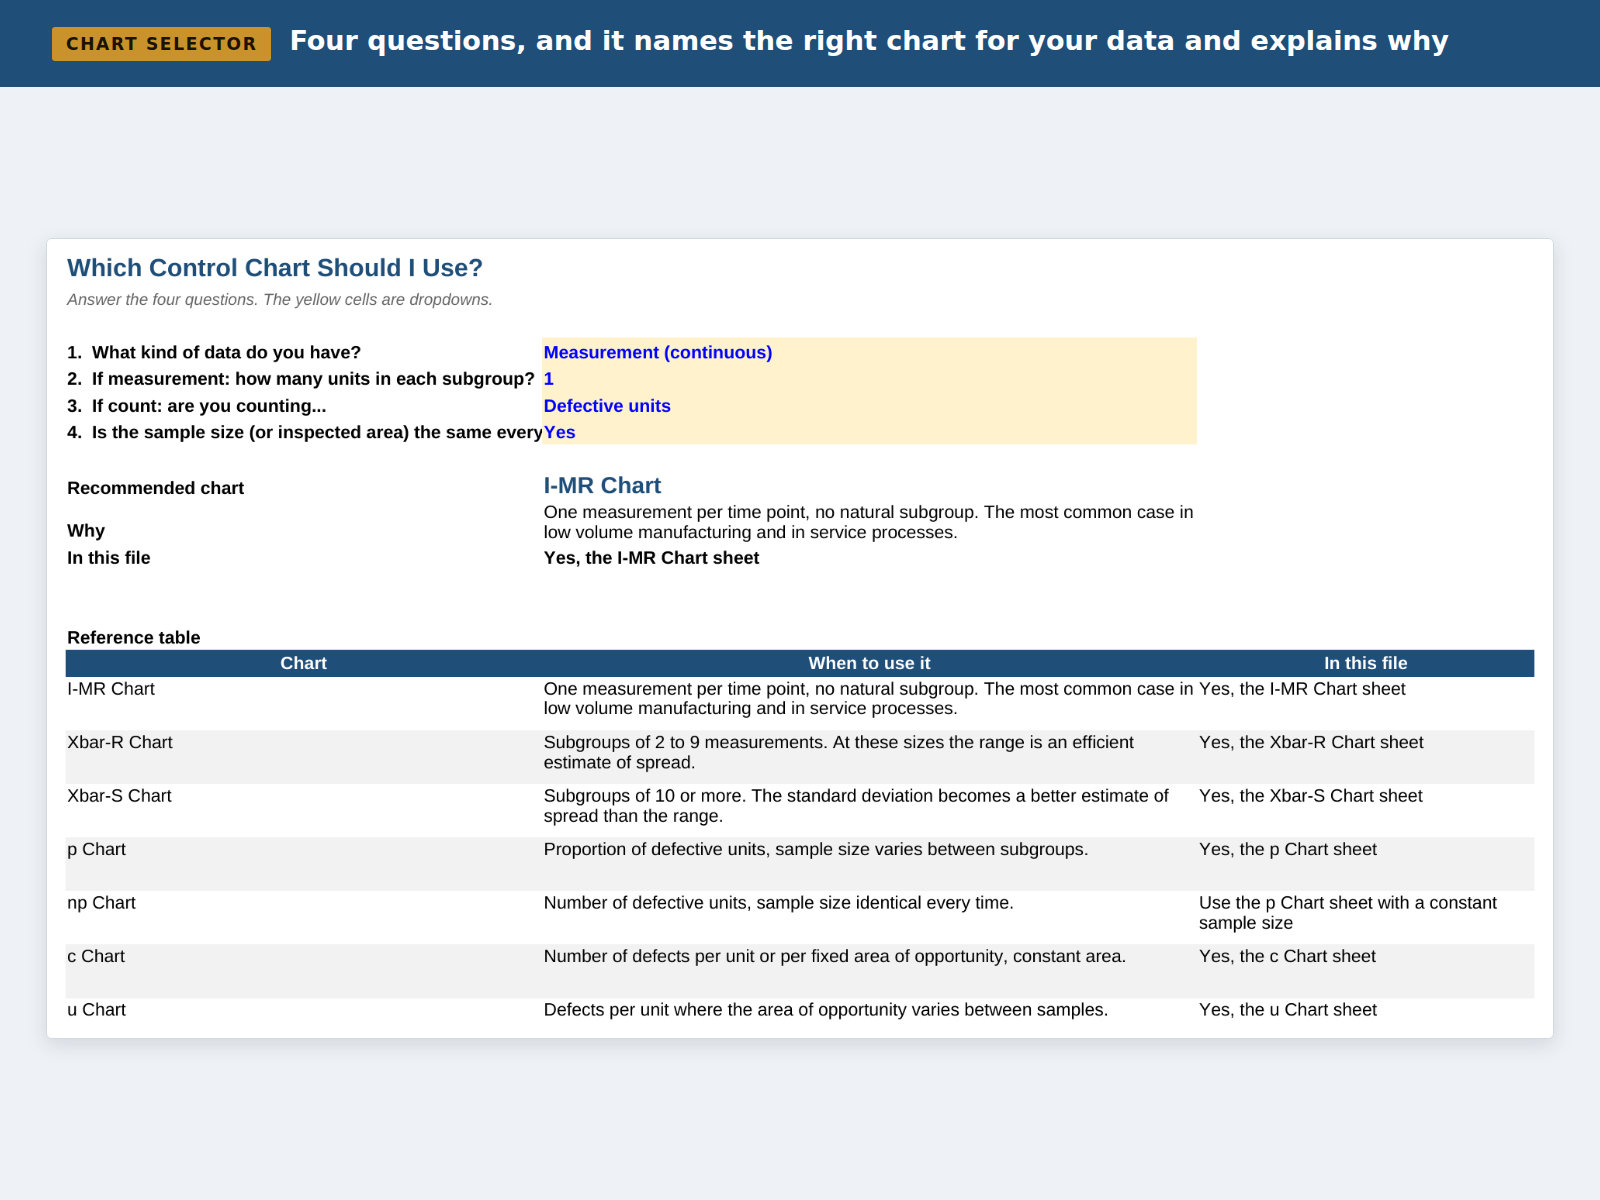
• Select the correct control chart for your data type and subgroup size, and justify the choice.
• Build a control chart with the correct constants applied automatically, without looking up a table.
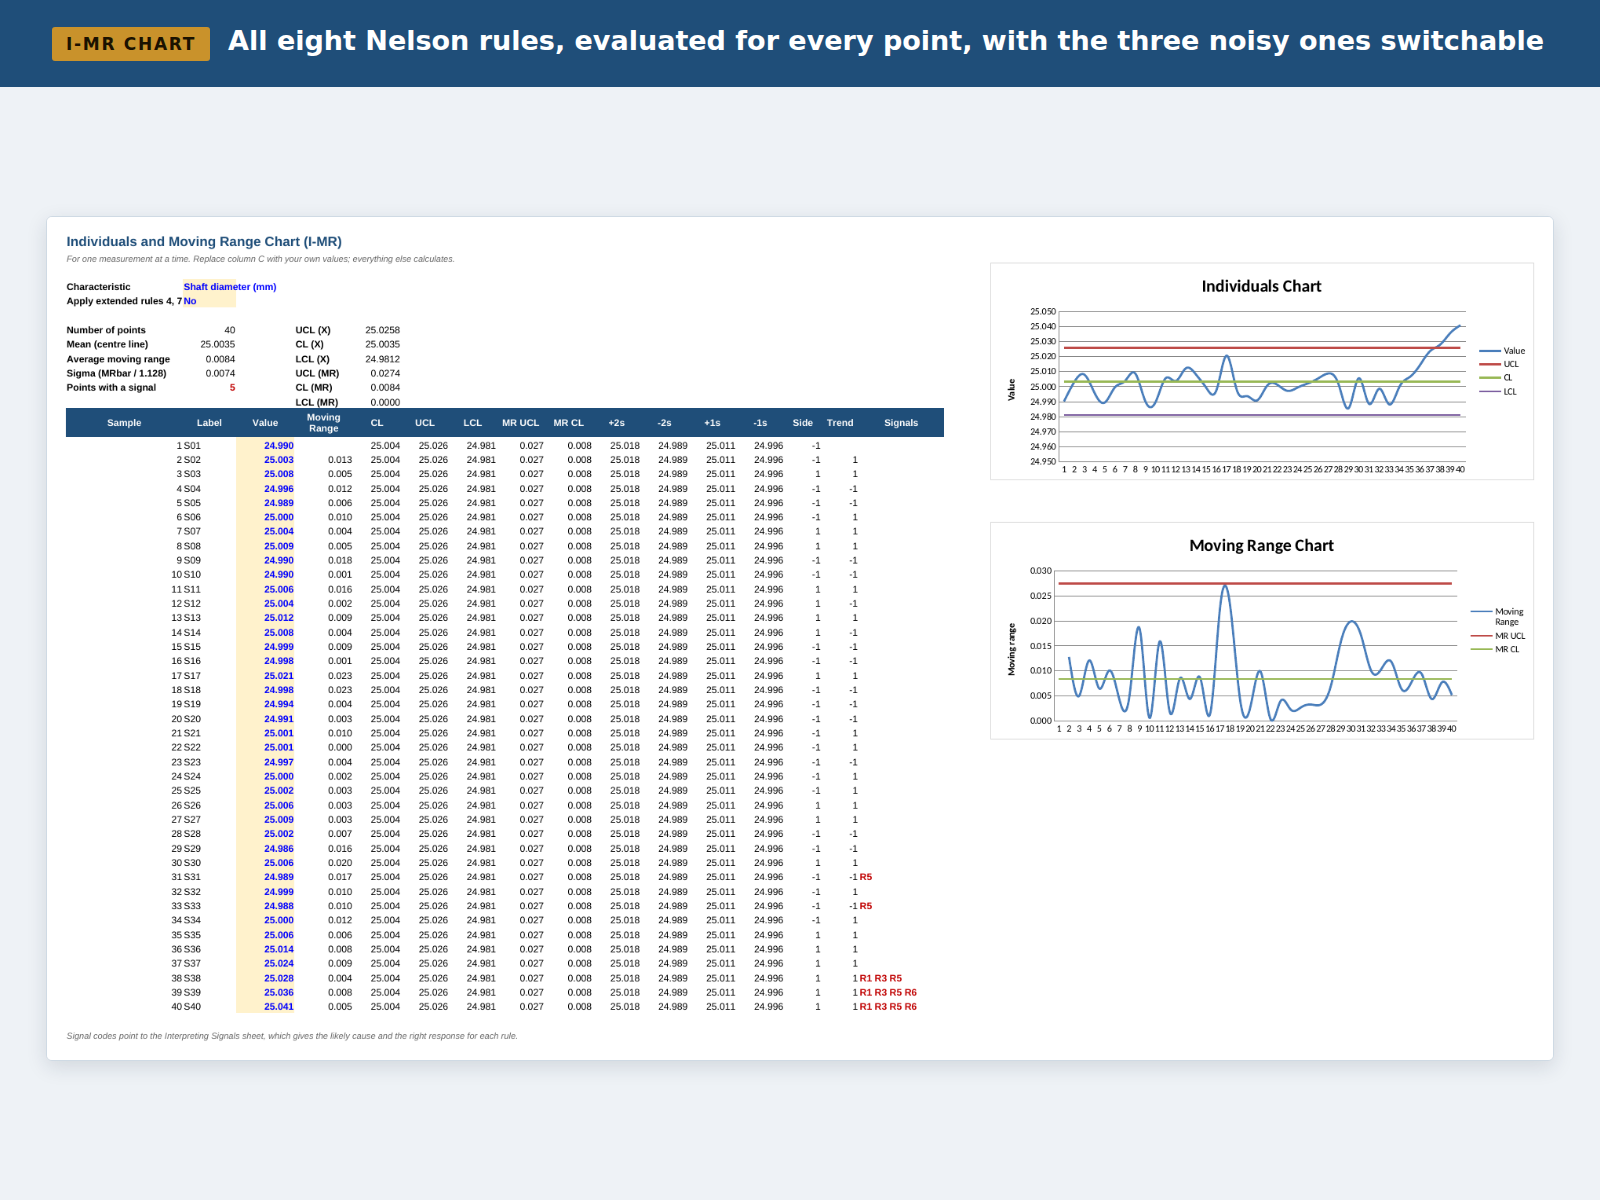
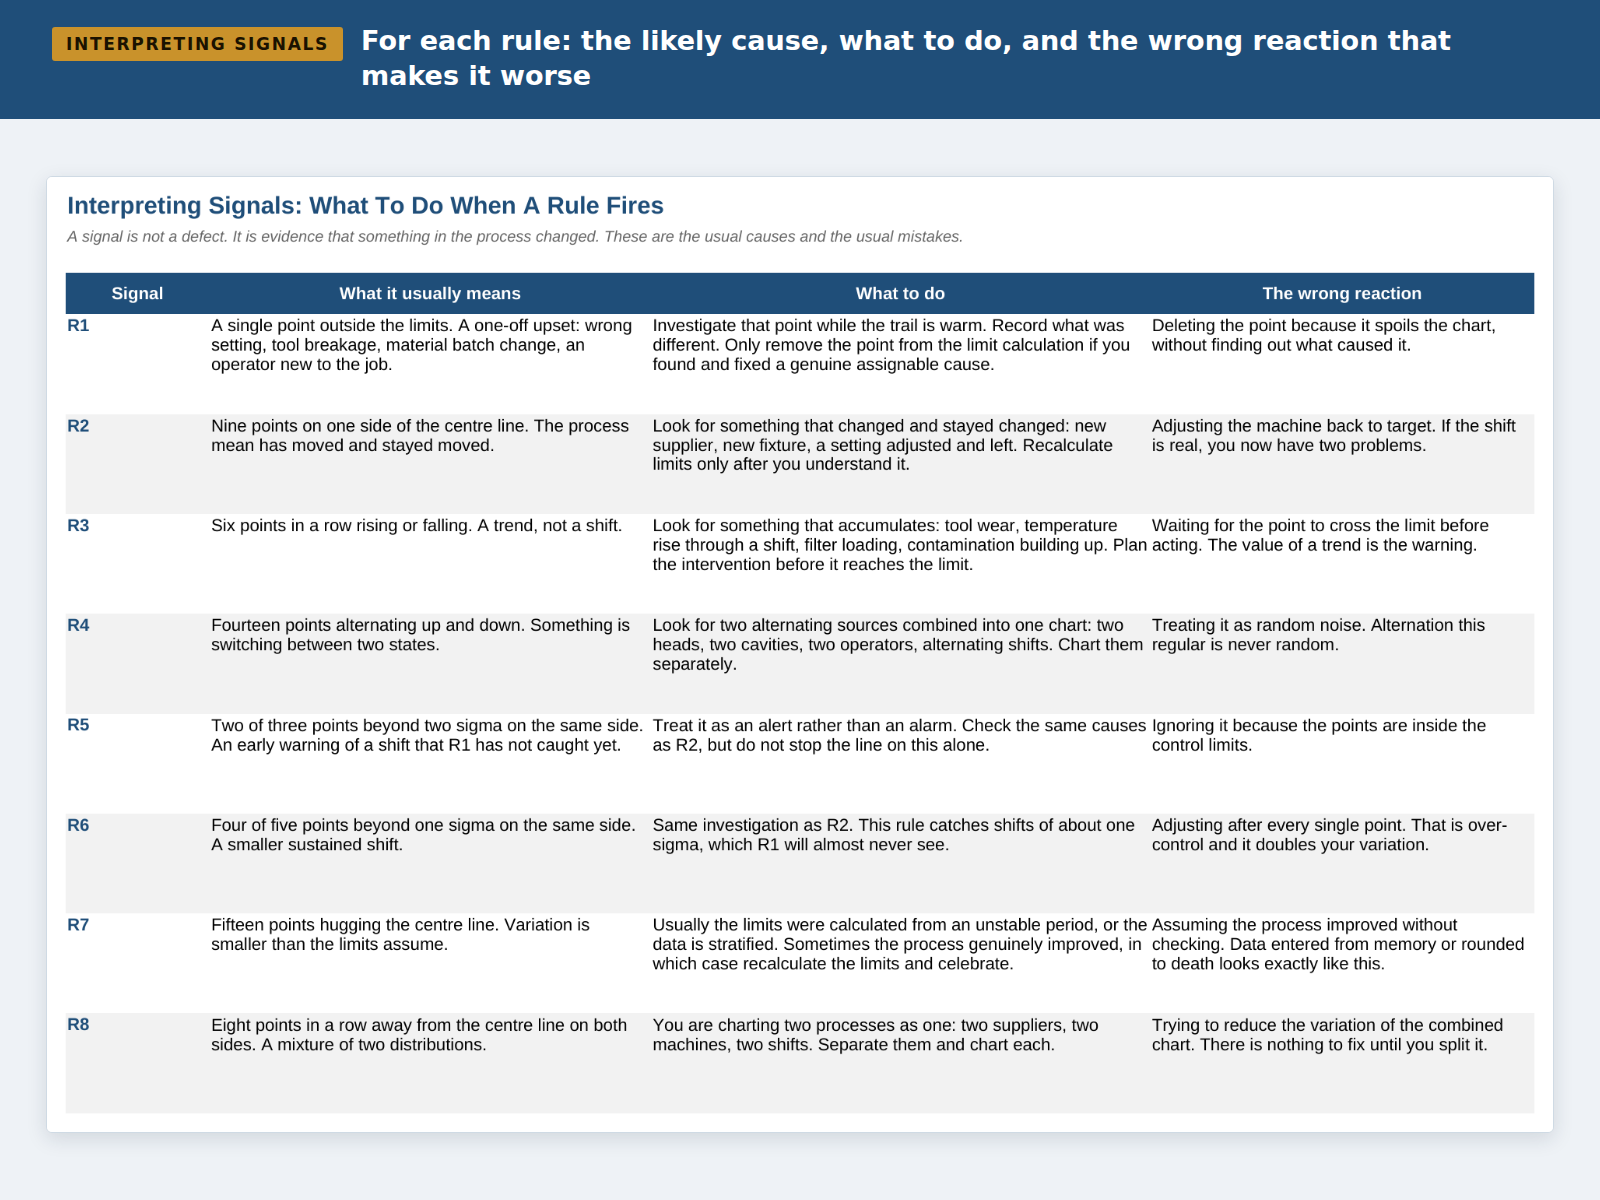
• Distinguish a genuine special cause from ordinary variation, using the eight Nelson rules, and decide which of them to apply.
• Respond to each type of signal correctly, and avoid the over-adjustment that increases variation.
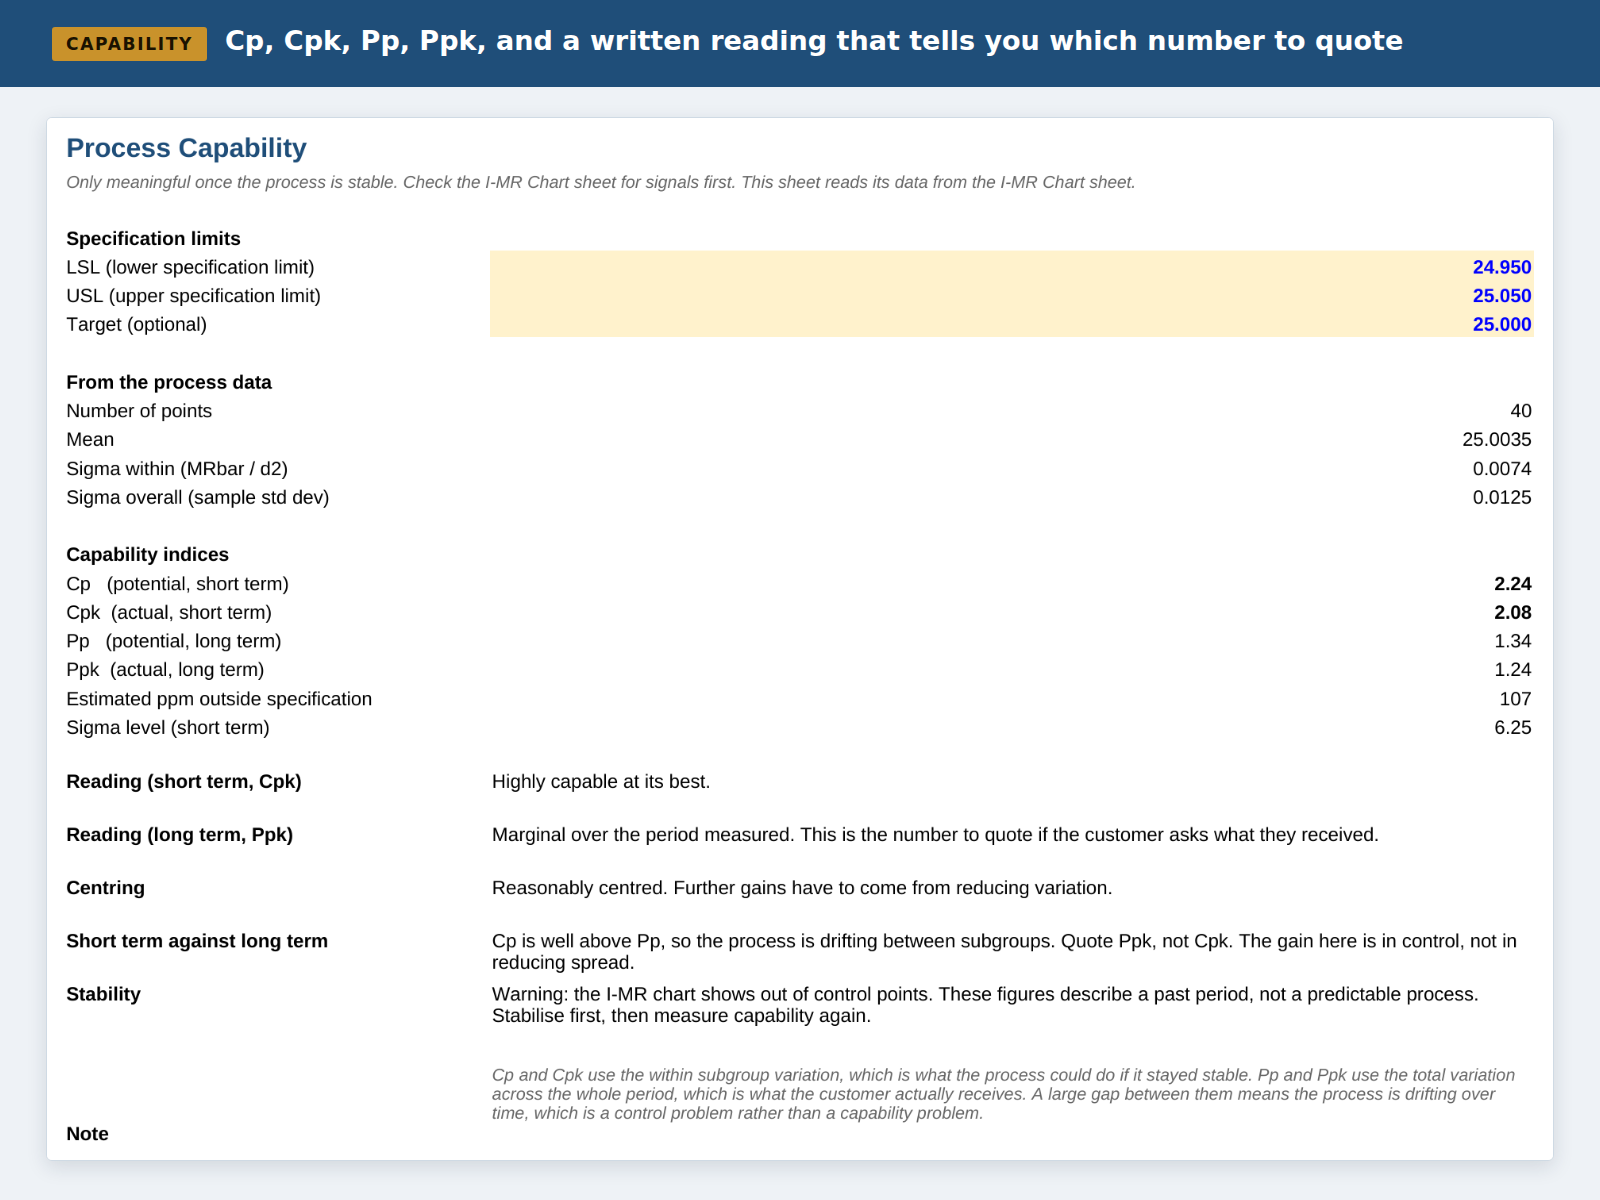
• Calculate Cp, Cpk, Pp and Ppk, and explain to a customer why the short term and long term figures differ.
• Recognise when a capability figure is meaningless because the process is not stable.
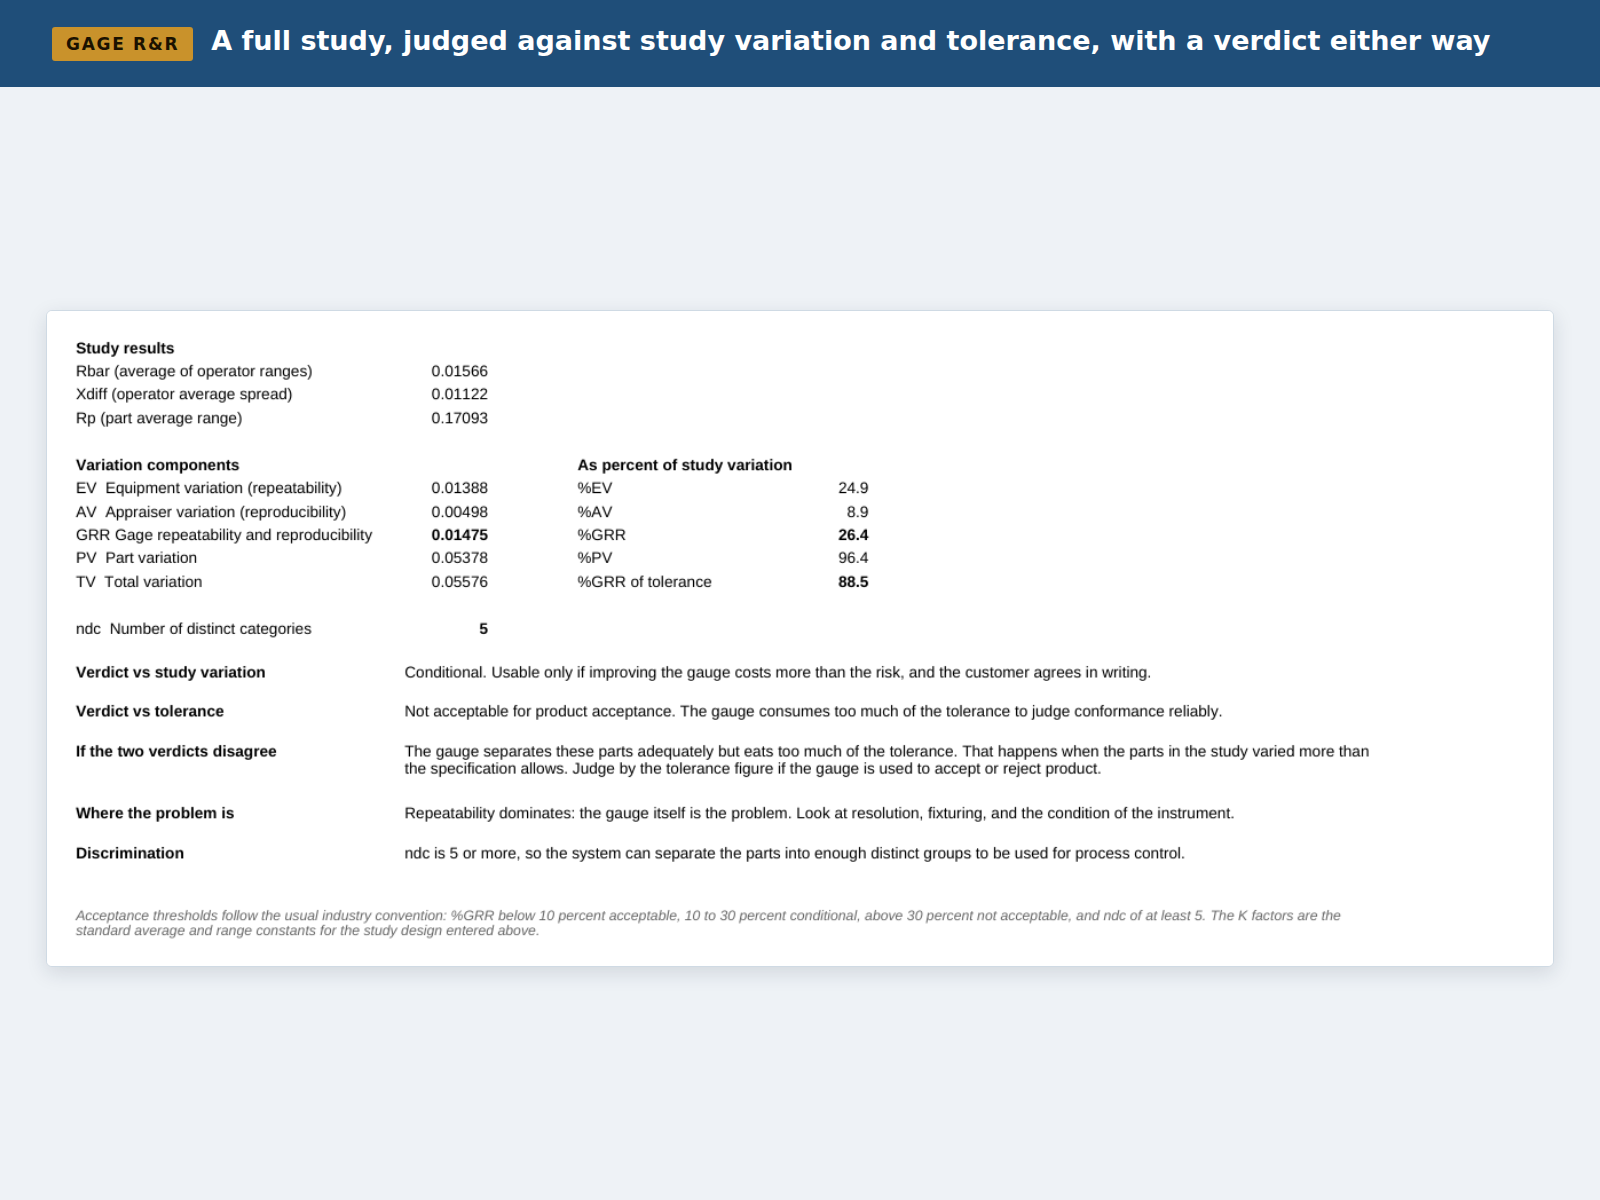
• Run and interpret a Gage R&R study, and judge the measurement system against both study variation and tolerance.
• Decide whether a measurement problem lies with the gauge or with the operators, and act accordingly.
• Manufacturing or laboratory processes with a measurable output, or with countable defects.
• Quality engineers, quality managers, Green Belts and Black Belts who need to do the analysis rather than teach it.
• Suppliers preparing capability or MSA evidence for IATF 16949, ISO 9001, VDA or a customer audit.
• Organisations that work in Excel and do not have, or do not want to pay for, a statistical package.
• Anyone who has been asked for a Cpk and is not certain the number they are about to send is defensible.
• Teams running a DMAIC project that has reached the Measure phase.
You want training slides to teach a class. This is a working tool, not a course. Most SPC material on the market is the other way round.
• You need automated data collection from a machine, a MES or a database. This is a workbook, and data is entered or pasted into it.
• You need an ANOVA Gage R&R, or a destructive, nested or attribute measurement study. This uses the average and range method, which is the AIAG standard for a normal repeatable study but does not separate the operator by part interaction.
• Your subgroups are larger than 25.
• You need hypothesis testing, regression, design of experiments or non-normal capability modelling. This workbook covers SPC, capability and MSA only.
• You are looking for a certified or validated system for a regulated release decision. This is a calculation aid and your own validation still applies.